Hot Sale 1330 CNC Router In China
Product Overview
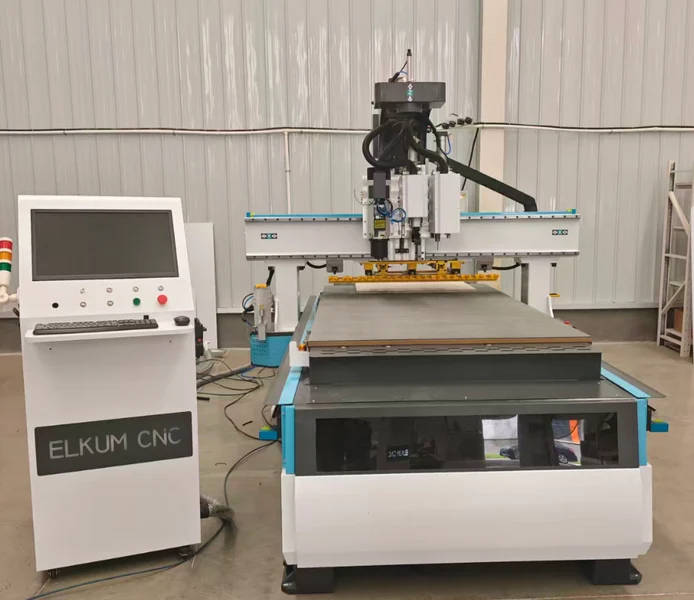
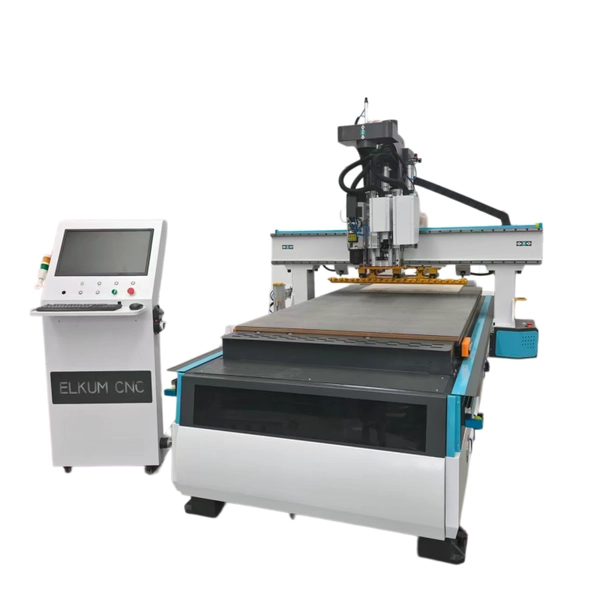
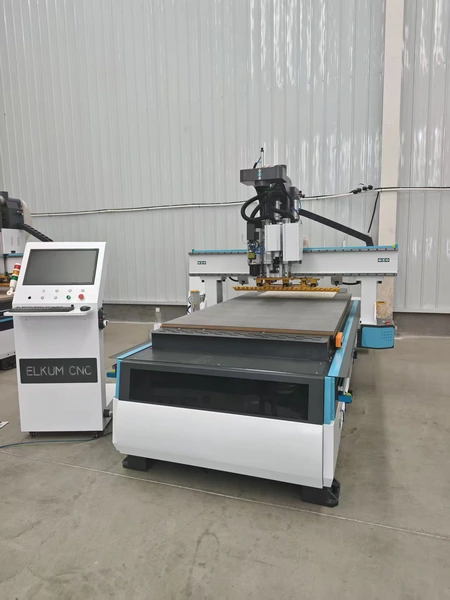
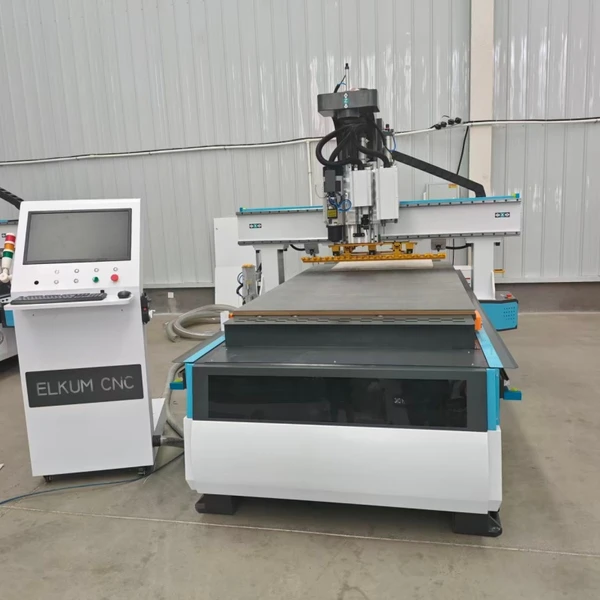
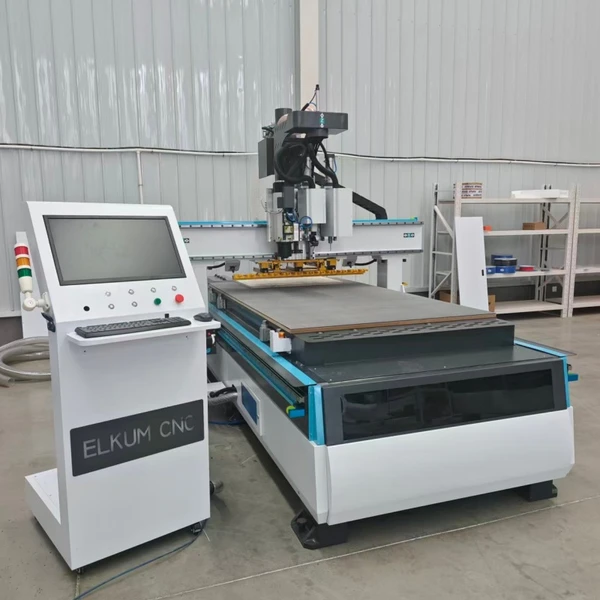
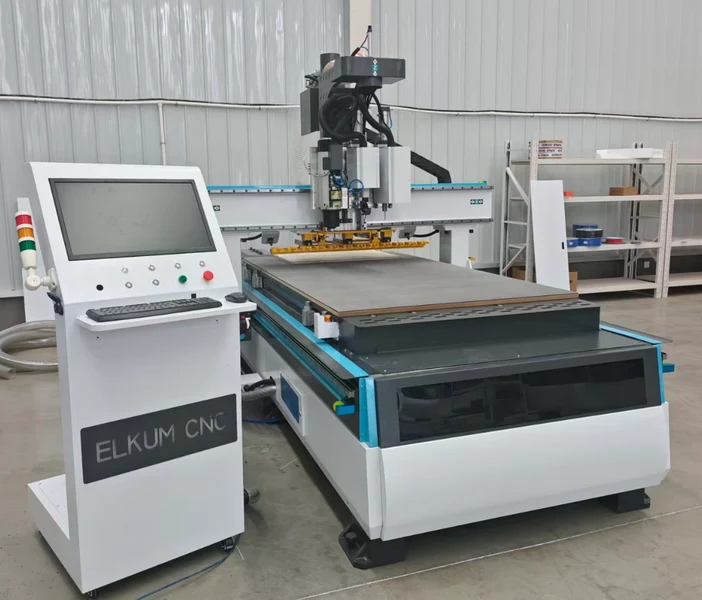
Model 1330 CNC Router is a gantry-moving 3-axis CNC processing machine supporting only X/Y/Z linear simultaneous motion with no rotary forming axes. Standard configuration includes water-cooled variable-frequency spindle, Weihong NcStudio / Xingduowei dedicated 3-axis control system. Suitable for cutting, relief carving, routing, grooving, drilling and engraving on non-metallic materials such as solid wood, MDF, multi-layer board, PVC and acrylic. Widely used in customized whole-house furniture, wooden-door factories, solid-wood furniture plants and wood-carving handicraft industries.
Six Core Advantages
- Robust Machine Frame: Integral heavy-gauge square-tube welded bed with high-temperature stress-relief tempering for long-term anti-deformation performance. Heavy-duty thickened gantry beam ensures vibration-free high-speed cutting.
- High-precision Transmission System: X/Y axes adopt high-precision helical-rack drive; Z-axis fitted with TBI ball screw. HIWIN 30 linear guideways from Taiwan deliver smooth travel with +/- 0.1 mm repeat positioning accuracy.
- High-power Air-cooled Spindle: Standard 9 kW air-cooled spindle, speed range 0-24,000 r/min. Delivers powerful cutting capacity, low noise and low temperature rise for deep-milling of hard wood.
- Dedicated 3-axis CNC System: Custom-built system with locked multi-axis expansion; no hardware interface for 4th/5th-axis upgrade. Matched with Weihong NcStudio / Xingduowei operation software supporting CAD import and G-code / NC file reading; user-friendly operation.
- Dual-mode Fixing Worktable: Combined T-slot aluminum profile + vacuum-adsorption table. Vacuum adsorption for thin sheets; fixture-bolt clamping for thick plates and irregular workpieces, effectively preventing workpiece shifting.
- Intelligent Automatic Lubrication: Micro-computer automatic oil-injection system feeds lubricant to screws and guide rails at preset intervals and dosage. Reduces manual maintenance and greatly extends service life of transmission components.
Technical Specifications
| Item | Specification |
| Model | 1330 CNC Router |
| Effective Travel | X: 1300 mm Y: 3000 mm Z: 200 mm |
| Simultaneous Axes | X/Y/Z 3-axis linear motion; no rotary axes; non-expandable to 4-/5-axis |
| Repeat Positioning Accuracy | ±0.05 mm |
| Spindle Motor | 9 kW Air-cooled Variable-frequency Spindle |
| Spindle Speed Range | 0-24 000 r/min |
| Toolholding Diameter | Φ3.175 / Φ4 / Φ6 / Φ12.7 mm |
| Drive System | 1 kW Weihong AC Servo Drive |
| Guideway / Screw | HIWIN 30 linear guideway (Taiwan); Z-axis TBI 3210 ball screw |
| Transmission Mode | X/Y: helical-rack drive; Z-axis: ball-screw drive |
| Control System | Weihong NcStudio / Xingduowei dedicated 3-axis system (multi-axis expansion locked) |
| Worktable Configuration | Vacuum adsorption + T-slot aluminum profile table |
| Lubrication System | Full-automatic micro-computer oil-injection system |
| Operating Voltage | 380 V / 50 Hz |
| Overall Dimension | 4600 × 2100 × 2100 mm |
| Machine Weight | 3100 KG |
| Compatible Materials | Solid wood, MDF, multi-layer board, PVC, acrylic, foam board |
| Supported File Formats | .nc, G-code, .plt, .eng |
Machine Structure Description of 1330 CNC Router
- Machine Bed Base: Integrally-welded heavy rectangular square-tube frame with high-temperature stress-relief tempering. Adjustable support feet at bottom for machine-level calibration.
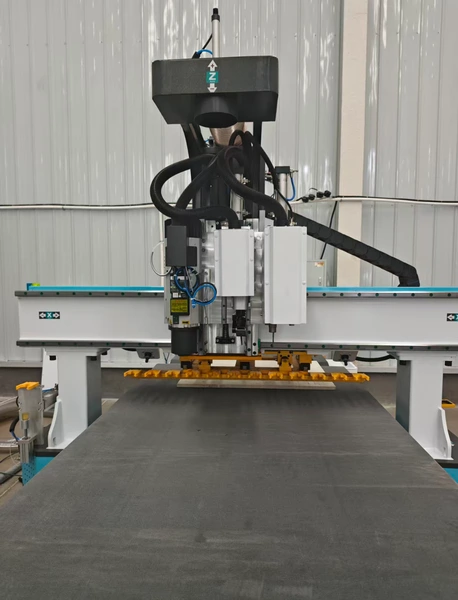
- Gantry Beam: Thick steel-plate monolithic structure with high rigidity to suppress vibration during high-speed cutting.
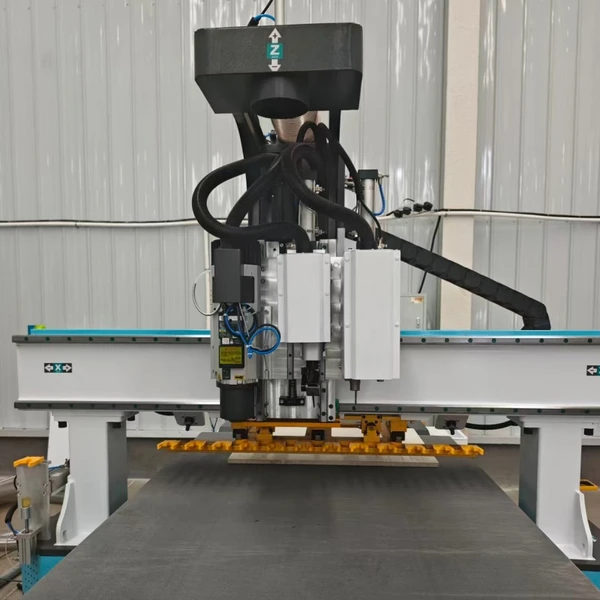
- 3-axis Motion Mechanism: X-axis: lateral head movement; Y-axis: longitudinal gantry travel; Z-axis: spindle head vertical movement for cutting.
- Air-cooled Spindle Unit: Core power unit for high-speed cutting; air-cooled design eliminates water-tank cooling requirements.
- Electrical Control Cabinet: Houses servo drives, frequency converter, switching power supply, control card, emergency-stop switch and main power switch.
- Vacuum-Adsorption Table: Multi-zone vacuum-adsorption structure matched with vacuum pump to prevent displacement of thin workpieces.
- Automatic Lubrication Unit: Timed and quantitative automatic oil supply to guide rails and ball screws.
- Operation Terminal: Industrial PC pre-installed with NcStudio 3-axis engraving control software.
Installation and Commissioning Procedures of 1330 CNC Router
Machine Positioning and Leveling
- Remove outer packaging and protective films. Place machine on flat hardened floor; reserve clearance >= 1 m around machine for operation and maintenance.
- Adjust adjustable feet at four corners. Calibrate worktable level with level gauge; overall level tolerance <= 0.02 mm/m.
- Lock foot fixing nuts to avoid machine offset during processing.
Water Circuit Installation
- Fill water tank with purified water; connect inlet/outlet hoses to spindle joints. Confirm no hose kinks or leakage.
- Apply 220 V power to water pump; test water circulation to ensure continuous unbroken flow.
Electrical Wiring
- Connect 3-phase 380 V industrial power supply; ensure reliable machine earthing.
- Connect communication data cable between PC and control cabinet. Verify secure connection of servo-motor and limit-switch wiring.
Lubricant Filling
- Fill automatic-lubrication tank with dedicated guide-rail lubricating oil.
- Manually jog three axes in idle motion; confirm uniform oil output on guide rails and ball screws.
System Commissioning
- Power-on, unlock emergency-stop button by rotation, start control system and execute Return-to-Mechanical-Home to calibrate axis coordinates.
- Run three-axis idle operation continuously for 10 minutes; check for abnormal noise, jamming or drifting.
- Mount test tool and perform tool-setting test. Verify accurate Z-axis downfeed with zero tool-collision risk.
Standard Complete Operating Procedure
Power-on Sequence
- Switch on workshop main power -> turn on cabinet main switch -> rotate to unlock red emergency-stop button.
- Start cooling-water pump and vacuum pump.
- Boot industrial PC and launch NcStudio 3-axis control software.
- In software menu: Machine -> Return to Mechanical Home for automatic axis zero-return coordinate calibration.
Tool Mounting and Workpiece Clamping
- Loosen collet with dedicated spindle wrench, insert engraving bit and tighten collet; confirm tool is free of wobble.
- Place workpiece on table: enable vacuum adsorption for thin sheets; use T-slot bolts plus clamps for thick / irregular parts. Ensure no warping or suspended workpiece sections.
Workpiece-origin Tool-setting
- Jog X/Y axes manually to lower-left starting point of workpiece; zero current X/Y coordinates.
- Jog Z-axis slowly down until tool tip lightly touches workpiece top surface; zero Z-axis coordinate to complete tool-setting.
Program Import and Simulation Verification
- Menu: File -> Load, open pre-processed NC / G-code machining file.
- Click Simulation to preview tool-path. Confirm cutting boundary stays within workpiece range and no gantry-collision risk. Close simulation after verification.
Machining Execution
- Set spindle speed and feed rate (refer to process-parameter table).
- Click Start Machining. Continuously observe cutting condition, chip evacuation and workpiece clamping status.
- Press emergency-stop button immediately upon abnormal noise, workpiece shift or tool breakage. Troubleshoot fault before resuming operation.
Shutdown Procedure
- After machining completion, raise Z-axis to safe height and stop spindle rotation.
- Shut down vacuum pump and cooling-water pump.
- Exit CNC software and turn off industrial PC.
- Switch off control-cabinet power and workshop main power.
- Clear wood chips from worktable; manually replenish lubricant for three axes.
Reference Machining-Process Parameters
| Material | Spindle Speed (r/min) | Feed Rate (mm/min) | Depth per Cut (mm) |
| Pine / Paulownia (softwood) | 16 000-18 000 | 1200-1500 | 1.0-1.5 |
| Oak / Walnut (hardwood) | 18 000-22 000 | 800-1000 | 0.6-1.0 |
| MDF | 20 000-22 000 | 1000-1300 | 1.2-1.8 |
| PVC Sheet | 22 000-24 000 | 700-900 | 1.0 |
| Acrylic Sheet | 22 000-24 000 | 600-800 | 0.8 |
Daily Maintenance Specifications
Daily Maintenance (Before Startup / After Shutdown)
- Clear wood chips and dust on worktable, guide rails and ball screws with brush and air gun.
- Inspect water-tank level and normal water-pump circulation.
- Confirm proper oil output of automatic-lubrication system; replenish dedicated lubricant when low.
- Inspect emergency-stop button, limit switches and cable jacket integrity for damage.
Weekly Maintenance
- Wipe guide rails and ball screws thoroughly; apply even coat of lubricating grease.
- Clean sediment inside water tank and replace circulating soft water.
- Check operating noise and abnormal heating of servo motors and spindle.
- Tighten all fixing bolts on gantry and worktable.
Monthly Maintenance
- Remove dust inside electrical cabinet; fasten all terminal connections.
- Inspect tension of timing belts and racks; belt sag shall not exceed 3 mm.
- Verify worktable level and re-adjust machine feet.
- Clean vacuum-pump filter element to guarantee sufficient vacuum adsorption force.
Long-term Shutdown Maintenance (Idle > 7 Days)
- Apply anti-rust lubricant to ball screws and guide rails; cover whole machine with dust cover.
- Drain all circulating water from cooling tank to prevent pipe cracking in low-temperature environments.
- Disconnect main power; store machine in dry moisture-proof environment.
Common Fault Diagnosis and Solutions
One axis cannot move
- Check loose or disconnected power and data connectors of corresponding servo drive.
- Swap drive connectors for testing; replace defective drive unit.
- In case of wire breakage or motor-coil failure, contact manufacturer after-sales service.
Spindle fails to rotate, abnormal noise or overheating
- Check frequency-converter error codes and confirm no three-phase power loss.
- Insufficient cooling-water flow or no water causes spindle overheating; clear water circuit and refill coolant.
- Spindle-bearing wear or coil burnout: return machine to factory for repair.
Dimensional deviation and workpiece offset during engraving
- Insufficient lubrication or chip jamming on racks / screws: clean dust and apply lubricant.
- Poor vacuum holding or loose clamps: re-secure workpiece.
- Loose transmission fasteners: tighten gantry and head connecting bolts.
- Re-execute Return-to-Mechanical-Home to recalibrate axis coordinates.
Frequent tool breakage
- Mismatched spindle speed and feed rate: adjust process parameters.
- Worn or poor-quality cutting tools: fit new carbide end-mills.
- Excessive Z-axis tool-setting error: perform precise tool-setting again.
- Knots or hard inclusions inside workpiece: reduce single-layer cutting depth.
Insufficient vacuum-adsorption force
- Vacuum-pump filter blocked: remove and clean filter element.
- Damaged table sealing strip: replace sealing strip.
- Workpiece warping causes air leakage: add auxiliary fixture clamping.
Safety Warning Instructions of 1330 CNC Router (Must Read)
General Safety Warnings
- The equipment is supplied with 380V/50Hz industrial power. Reliable earthing is mandatory; ground wire shall be copper cable >= 4 mm2. Neutral-ground common connection is prohibited to prevent electrostatic damage to the control system and electric shock hazards.
- Wear dust-proof respirator and safety goggles throughout operation. Wood dust may cause respiratory injury. Never clean rotating spindle and wood chips by hand; use only brushes or air guns for cleaning.
- The red emergency-stop button on the machine body is for emergency shutdown. Press it immediately in case of tool collision, abnormal noise, electric leakage or loose workpiece. Rotate clockwise to unlock for reset.
- Do not open the electrical cabinet or reach into the processing zone while the machine is running. Keep body and clothing away from the high-speed rotating spindle.
- Minors and untrained personnel are forbidden to operate this machine independently. Operators must fully read this manual before operation.
- The workshop shall be equipped with dust-removal facilities. Accumulated wood dust may cause fire. Clean worktable, guide rails and internal dust inside electrical cabinet before daily shutdown.
Export Compliance Safety (Dual-Use Item Control)
This machine is a pure 3-axis linear simultaneous-motion device without A/C rotary axes. CNC system hardware and firmware lock 4th/5th-axis expansion. Factory-set positioning accuracy >= 0.01 mm. It does not fall under the control scope of Dual-Use Item 2B201, so a Dual-Use Item Export License is not required for export.
For overseas sales, retain customer end-use commitment letters and sales records for no less than 5 years. Resale or lending of this equipment to military or defense-related organizations is strictly prohibited.